At Manfisa Welding Products, we are committed not only to supplying premium-quality products, but also to providing the expertise and support needed to ensure efficient, reliable, and safe welding operations.
Aluminium is a lightweight metal with a density of approximately 2.7 kg/dm³. It has a silvery appearance and is relatively soft, depending on the alloy used and in comparison with other metals commonly employed in industrial applications.
Among its technological characteristics, the most important factors to consider in welding applications are its low density, high thermal conductivity, the presence of an aluminium oxide (Al₂O₃) layer, its high susceptibility to porosity formation in the deposited weld metal, and, finally, its relatively low mechanical strength.
The low density of aluminium offers a significant advantage when welding in PF, PD and even PE positions. In these positions, gravity is less likely to cause the molten metal in the weld pool to drip or fall away, making it possible to weld aluminium with fewer difficulties.
However, in any welding position, aluminium’s low density can also present a challenge. When the molten weld pool is located between the electric arc and the joint, fusion of the base metal may be impaired, leading to the defect known as lack of fusion. This occurs because the base material is not being directly heated by the electric arc, and melting must therefore take place through contact with the molten filler metal. Due to its low density, the molten metal exerts little pressure on the base material, reducing the likelihood of achieving proper fusion.
To prevent this issue, the electric arc should be positioned slightly ahead of the weld pool, allowing the arc itself to melt the joint while the filler metal forms the weld bead.
This defect becomes more likely as the weld pool size decreases. In practical welding terms, the lower the heat input, the greater the risk of lack of fusion.

This characteristic means that, once the electric arc is established on the joint, a certain amount of time passes before the material begins to melt. Although aluminium has a relatively low melting point compared with other weldable metals, the heat introduced by the electric arc is rapidly dissipated through the plate or component being welded. This effect becomes more pronounced as the thickness of the material increases.
Likewise, aluminium’s high thermal conductivity makes the start of the welding process both in GMAW (MIG) and GTAW (TIG) particularly susceptible to lack of fusion or incomplete penetration defects.
Esto no es un problema en la soldadura GTAW-TIG, puesto que el operario es quien decide cuándo comenzar con la aportación del metal una vez se establece el arco eléctrico.
This issue is generally less critical in GTAW (TIG) welding, since the welder can decide when to begin adding filler metal after the electric arc has been established.
In GMAW (MIG) welding, however, the electric arc and filler metal are introduced simultaneously. As a result, molten filler metal may be deposited onto relatively cold base material, increasing the risk of lack of fusion or incomplete penetration at the start of the weld bead.
This phenomenon is more pronounced when welding thicker sections due to their greater capacity to dissipate heat.
Several solutions can be used to minimize this problem:
- a) Preheat the components before welding.
- b) Start the weld outside the joint and then move into the joint immediately afterwards (this normally requires slight grinding of the weld start area outside the actual joint).
- c) Place an aluminium run-on tab adjacent to the joint, start welding on the tab, and then continue into the actual weld joint.
- d) Other solutions developed by equipment manufacturers or welding engineers.
Special attention should also be given to the joining of weld beads. In this case, the recommended practice is to grind the end of the previous weld bead at an angle, creating a run-on ramp. The new weld should begin on this ramp and then continue into the previous bead. This ensures that any lack of fusion remains localized on the surface of the previous weld bead. A final grinding operation can then be performed to remove excess material and eliminate the defect.
The melting point of alumina (Al₂O₃) is significantly higher than that of aluminium itself: approximately 2,062°C, compared with aluminium’s typical melting point of around 660°C.
For this reason, the oxide layer should be removed prior to welding by mechanical means, typically through brushing with a stainless steel wire brush dedicated to aluminium applications.
In GTAW (TIG) welding, alternating current (AC) is generally preferred, as it helps break up and remove the oxide layer during the welding process.
Aluminium welding is highly susceptible to the formation of porosity in the deposited weld metal. The most common cause is the presence of hydrogen (H₂).
Even very low concentrations of hydrogen, measured in parts per million (ppm), can lead to porosity and are therefore considered one of the primary causes of this defect.
For this reason, special attention must be paid to factors such as air drafts in the welding area, atmospheric humidity, moisture on the workpieces, improper storage of welding wire, moisture contamination of the wire itself, and gases used during preheating (the use of propane is not recommended). In addition, any contamination that may release hydrogen during combustión such as cutting fluids, oils, lubricants, or other residues must be carefully avoided.
Aluminium can generally be considered a relatively soft metal.
As a result, aluminium shavings may be generated if the wire feed system of a GMAW (MIG) welding machine is not in good condition, if unsuitable drive rolls are used, or if the drive roll pressure is excessive. These aluminium particles can be carried by the wire into the liner, eventually causing feeding problems or blockages.
The liner inside the welding torch should be specifically designed for aluminium and have an internal diameter that allows the filler wire to pass smoothly with minimal resistance.
The contact tip must also be suitable for aluminium welding applications.
Risks During Handling:
- The beginning and end of the welding wire may cause injury.
- Dropping spools may result in impact injuries.
- Improper storage may lead to collapsed stacks.
- Stacked spools can become unstable and may cause accidents or injuries.
Recommended Safety Measures:
- The use of protective gloves is recommended when handling spools.
- The use of safety footwear is recommended.
- Do not stack spools outside their original packaging.
Operating instructions should always be available wherever spools are handled.
In addition to the recommendations provided in these instructions, all applicable local safety regulations must be observed.
The manufacturer accepts no liability for damage resulting from improper handling or misuse of the supplied material.
It is recommended to use the material within 18 months of receipt, provided it remains in its original packaging and is stored in a clean, dry environment protected from moisture and contamination. Once the package has been opened, and if the entire quantity is not used, the remaining material should be kept in its original box, securely closed, and preferably stored in a heated cabinet or controlled environment at a temperature of at least 20°C. Avoid contamination of the welding wire with any foreign substances.
When releasing the wire to feed it into the welding machine, a spring-back effect may occur, causing the outer wire loops to expand from their position on the spool. To prevent this, we recommend holding the outer loops firmly by hand before attaching the wire to the machine.
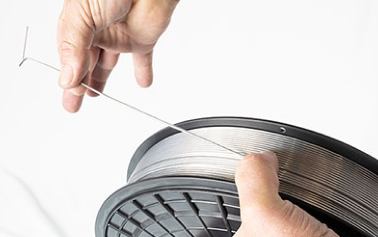
Avoid crossing or tangling the wire during machine feeding, as this can cause serious wire-feeding problems and affect the proper operation of the equipment.
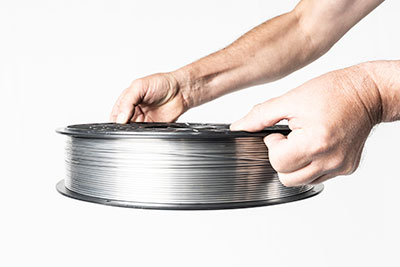
Avoid dropping spools during handling, as this may damage or break the spool. Particular care should be taken when handling IRU 320 spools.
YES
NO
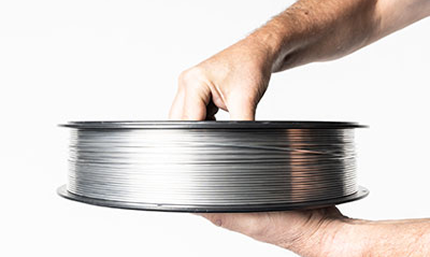
Plastic spools are reusable and/or recyclable waste materials, while the packaging materials are recyclable.
It is the responsibility of the end user to manage and dispose of these materials appropriately in accordance with European Directive 94/62/EC on Packaging and Packaging Waste.