THE RIGHT ALLOY FOR OPTIMUM PERFORMANCE
At Manfisa Welding Products, we offer a comprehensive range of aluminium alloys to ensure the best solution for every application. Choosing the right alloy improves weld quality, optimizes production processes, and maximizes productivity. Contact us, and we will help you find the best option for your needs.
M4043
Aluminium-Silicon solid welding wire for GMAW (MIG) and GTAW (TIG) welding of aluminium alloys.
Provides an excellent surface finish. When used with 6000 series aluminium alloys, it offers high resistance to weld cracking. Ideal for metal fabrication, bicycles, motorcycles, automotive components, and ventilation systems.
EN ISO 18273 | S Al 4043 (AlSi5) |
|---|---|
AWS/SFA-5.10/5.10M | ER 4043 |
UNS | A94043 |
ISO TR 17671-4 / EN 1011-4 | Type 4 |
ASME IX | F-Nº23 (QW-432) |
Vd TÜV 1153 | DB N. 61.254.01 | CE N. 0035-CPR-C616 |
|---|
Requirements according to EN ISO 18273. The individual values shown in the table are maximum values.
Si | Fe | Cu | Mn | Mg | Zn | Ti | Be | Al |
|---|---|---|---|---|---|---|---|---|
4,5-6,0 | 0,60 | 0,30 | 0,15 | 0,20 | 0,10 | 0,15 | 0,0003 | Rest./Bal. |
The mechanical properties of the deposited weld metal are influenced by dilution with the base material.
Gas | Temp. | Condition | 0.2% Yield Strength | Tensile Strength | Elongation | |
|---|---|---|---|---|---|---|
Values according to DIN 1732-3 | I1 | 20ºC | Typical As-Welded | ≥ 120 N/mm2 | ≥ 250 N/mm2 | ≥ 18% |
Suitable for welding cast aluminium alloys and for joining cast aluminium components to products made from 3000, 5000, 6000 and 7000 series aluminium alloys. Also suitable for welding products made from 3000, 5000 and 6000 series aluminium alloys.
Product | Diameter (Ø mm) |
|---|---|
Plastic spools, basket spools and packs | GMAW: 1.20 - 1.60 mm GTAW: 2.4 - 3.2 mm |
Store in a clean, dry environment protected from moisture and contamination. After opening the package, if the material is not used completely, keep it in its original closed packaging and preferably in a heated storage cabinet at a temperature of at least 20°C (68°F). The spool label (GMAW) or package label (GTAW) should be retained for product traceability
Remove the aluminium oxide layer, contaminants (grease, dust, etc.), and moisture from the welding area by mechanical cleaning or brushing with a stainless steel wire brush. Do not machine bevels using oil-based lubricants.
For GMAW (MIG) welding, wire guides (liners, conduits, etc.) and drive rolls must be suitable for aluminium applications and maintained in a clean condition. Avoid striking the gas nozzle.
Thickness | Temperature | |
|---|---|---|
Preheating | ≥ 10 mm | Initial: 90-110ºC |
Interpass Temperature | All thicknesses | Max. 110ºC |
Inert Gas: 100% Ar, Ar-He mixture
EN ISO 14175: I1
Gas Flow Rate: 14-18 L/min. Waste shall be properly managed in accordance with Directive 94/62/EC.
 |  |  |  |  |  | |
|---|---|---|---|---|---|---|
EN ISO 6947 | PA | PB | PC | PD | PE | PF |
ASME IX | 1G | 2F | 2G | 4F | 4G | 3G ↑ |
GMAW: Direct current, electrode positive (DCEP / DC+). Applicable in both pulsed and non-pulsed transfer modes.
GTAW: Alternating current (AC). Applicable in both pulsed and non-pulsed welding modes.
These parameters may vary depending on the power source and welding procedure used.
ø 1,0 mm
Union | Param.* | Welding positions | |
|---|---|---|---|
All positions | |||
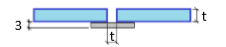 | BW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
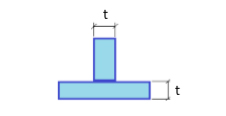 | FW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
ø 1,2 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t ≤ 3mm | Int. (A) | 140-150 | - | 140-150 | - | 140-150 | 130-140 |
Volt. (V) | 21-22 | - | 21-22 | - | 21-22 | 21-23 | ||
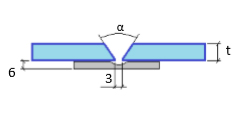 | BW mb t > 3mm t ≤ 8mm | Int. (A) | 160-180 | - | 150-170 | - | 150-170 | 140-160 |
Volt. (V) | 22-24 | - | 21-23 | - | 21-23 | 23-24 | ||
BW mb t > 8mm | Int. (A) | 180-220 | - | 170-180 | - | 180-220 | 140-200 | |
Volt. (V) | 23-25 | - | 23-24 | - | 23-25 | 23-24 | ||
| FW t ≤ 3mm | Int. (A) | 130-140 | |||||
Volt. (V) | 21-23 | |||||||
FW t > 3mm t ≤ 8mm | Int. (A) | 150-170 | ||||||
Volt. (V) | 21-23 | |||||||
FW t > 8mm | Int. (A) | 180-220 | 170-190 | 200-220 | 200-220 | 140-180 | ||
Volt. (V) | 23-25 | 23-24 | 23-25 | 23-25 | 23-24 | |||
ø 1,6 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||
| FW t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||

M5356
Aluminium-Magnesium solid welding wire for GMAW (MIG) and GTAW (TIG) welding of aluminium alloys.
Recommended for applications requiring high tensile strength. The most commonly used welding alloy within the Aluminium-Magnesium (Al-Mg) family.
EN ISO 18273 | Al 5356 (Al Mg5Cr(A)) |
|---|---|
AWS/SFA-5.10/5.10M | ER 5356 |
UNS | A95356 |
ISO TR 17671-4 / EN 1011-4 | Type 5 |
ASME IX | F-Nº22 (QW-432) |
Vd TÜV 1153 | DB N. 61.254.01 | CE N. 0035-CPR-C616 |
|---|
Requirements according to EN ISO 18273. The individual values shown in the table are maximum values.
Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti | Be | Al |
|---|---|---|---|---|---|---|---|---|---|
0,25 | 0,40 | 0,10 | 0,05-0,20 | 4,5-5,5 | 0,05-0,20 | 0,10 | 0,06-0,20 | 0,0003 | Rest./Bal. |
The mechanical properties of the deposited weld metal are influenced by dilution with the base material.
Gas | Temp. | Condition | 0.2% Yield Strength | Tensile Strength | Elongation | |
|---|---|---|---|---|---|---|
Values according to DIN 1732-3 | I1 | 20ºC | As welded | ≥ 120 N/mm2 | ≥ 250 N/mm2 | ≥ 18% |
Recommended for welding aluminium alloys of the 5000 and 6000 series.
Product | Diameter (Ø mm) |
|---|---|
Plastic spools, basket spools and packs | GMAW: 1.20 - 1.60 mm GTAW: 2.4 - 3.2 mm |
Store in a clean, dry environment protected from moisture and contamination. After opening the package, if the material is not used completely, keep it in its original closed packaging and preferably in a heated storage cabinet at a temperature of at least 20°C (68°F). The spool label (GMAW) or package label (GTAW) should be retained for product traceability.
Remove the aluminium oxide layer, contaminants (grease, dust, etc.), and moisture from the welding area by mechanical cleaning or brushing with a stainless steel wire brush. Do not machine bevels using oil-based lubricants.
For GMAW (MIG) welding, wire guides (liners, conduits, etc.) and drive rolls must be suitable for aluminium applications and maintained in a clean condition. Avoid striking the gas nozzle.
Thickness | Temperature | |
|---|---|---|
Preheating | ≥ 10 mm | Initial: 90-110ºC |
Interpass Temperature | All thicknesses | Max. 110ºC |
Inert Gas: 100% Ar, Ar-He mixture
EN ISO 14175: I1
Gas Flow Rate: 14-18 L/min
| | | | | | |
|---|---|---|---|---|---|---|
EN ISO 6947 | PA | PB | PC | PD | PE | PF |
ASME IX | 1G | 2F | 2G | 4F | 4G | 3G ↑ |
GMAW: Direct current, electrode positive (DCEP / DC+). Applicable in both pulsed and non-pulsed transfer modes.
GTAW: Alternating current (AC). Applicable in both pulsed and non-pulsed welding modes.
These parameters may vary depending on the power source and welding procedure used.
ø 1,0 mm
Union | Param.* | Welding positions | |
|---|---|---|---|
All positions | |||
| BW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
| FW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
ø 1,2 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t ≤ 3mm | Int. (A) | 140-150 | - | 140-150 | - | 140-150 | 130-140 |
Volt. (V) | 21-22 | - | 21-22 | - | 21-22 | 21-23 | ||
| BW mb t > 3mm t ≤ 8mm | Int. (A) | 160-180 | - | 150-170 | - | 150-170 | 140-160 |
Volt. (V) | 22-24 | - | 21-23 | - | 21-23 | 23-24 | ||
BW mb t > 8mm | Int. (A) | 180-220 | - | 170-180 | - | 180-220 | 140-200 | |
Volt. (V) | 23-25 | - | 23-24 | - | 23-25 | 23-24 | ||
| FW t ≤ 3mm | Int. (A) | 130-140 | |||||
Volt. (V) | 21-23 | |||||||
FW t > 3mm t ≤ 8mm | Int. (A) | 150-170 | ||||||
Volt. (V) | 21-23 | |||||||
FW t > 8mm | Int. (A) | 180-220 | 170-190 | 200-220 | 200-220 | 140-180 | ||
Volt. (V) | 23-25 | 23-24 | 23-25 | 23-25 | 23-24 | |||
ø 1,6 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||
| FW t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||
M5183
Aluminium-Magnesium solid welding wire for GMAW (MIG) and GTAW (TIG) welding of aluminium alloys.
High tensile strength welds, high toughness, and excellent resistance to seawater corrosion. Railway, shipbuilding, offshore, and cryogenic tank applications.
EN ISO 18273 | Al 5183 (Al Mg4,5 Mn0,7(A)) |
|---|---|
AWS/SFA-5.10/5.10M | ER 5183 |
UNS | A95183 |
ISO TR 17671-4 / EN 1011-4 | Type 5 |
ASME IX | F-Nº22 (QW-432) |
Vd TÜV 1153 | DB N. 61.254.01 | CE N. 0035-CPR-C616 |
|---|
Requirements according to EN ISO 18273. The individual values shown in the table are maximum values.
Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti | Be | Al |
|---|---|---|---|---|---|---|---|---|---|
0,40 | 0,40 | 0,10 | 0,05-1,0 | 4,3-5,2 | 0,05-0,25 | 0,15 | 0,06-0,20 | 0,0003 | Rest./Bal. |
The mechanical properties of the deposited weld metal are influenced by dilution with the base material.
Gas | Temp. | Condition | 0.2% Yield Strength | Tensile Strength | Elongation | |
|---|---|---|---|---|---|---|
Values according to DIN 1732-3 | I1 | 20ºC | As welded | ≥ 130 N/mm2 | ≥ 275 N/mm2 | ≥ 18% |
Suitable for welding 5000 and 6000 series aluminium alloys.
Product | Diameter (Ø mm) |
|---|---|
Plastic spools, basket spools and packs | GMAW: 1.20 - 1.60 mm GTAW: 2.4 - 3.2 mm |
Store in a clean, dry environment protected from moisture and contamination. After opening the package, if the material is not used completely, keep it in its original closed packaging and preferably in a heated storage cabinet at a temperature of at least 20°C (68°F). The spool label (GMAW) or package label (GTAW) should be retained for product traceability.
Remove the aluminium oxide layer, contaminants (grease, dust, etc.), and moisture from the welding area by mechanical cleaning or brushing with a stainless steel wire brush. Do not machine bevels using oil-based lubricants.
For GMAW (MIG) welding, wire guides (liners, conduits, etc.) and drive rolls must be suitable for aluminium applications and maintained in a clean condition. Avoid striking the gas nozzle.
Thickness | Temperature | |
|---|---|---|
Preheating | ≥ 10 mm | Initial: 90-110ºC |
Interpass Temperature | All thicknesses | Max. 110ºC |
Inert Gas: 100% Ar, Ar-He mixture
EN ISO 14175: I1
Gas Flow Rate: 14-18 L/min
| | | | | | |
|---|---|---|---|---|---|---|
EN ISO 6947 | PA | PB | PC | PD | PE | PF |
ASME IX | 1G | 2F | 2G | 4F | 4G | 3G ↑ |
GMAW: Direct current, electrode positive (DCEP / DC+). Applicable in both pulsed and non-pulsed transfer modes.
GTAW: Alternating current (AC). Applicable in both pulsed and non-pulsed welding modes.
These parameters may vary depending on the power source and welding procedure used.
ø 1,0 mm
Union | Param.* | Welding positions | |
|---|---|---|---|
All positions | |||
| BW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
| FW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
ø 1,2 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t ≤ 3mm | Int. (A) | 140-150 | - | 140-150 | - | 140-150 | 130-140 |
Volt. (V) | 21-22 | - | 21-22 | - | 21-22 | 21-23 | ||
| BW mb t > 3mm t ≤ 8mm | Int. (A) | 160-180 | - | 150-170 | - | 150-170 | 140-160 |
Volt. (V) | 22-24 | - | 21-23 | - | 21-23 | 23-24 | ||
BW mb t > 8mm | Int. (A) | 180-220 | - | 170-180 | - | 180-220 | 140-200 | |
Volt. (V) | 23-25 | - | 23-24 | - | 23-25 | 23-24 | ||
| FW t ≤ 3mm | Int. (A) | 130-140 | |||||
Volt. (V) | 21-23 | |||||||
FW t > 3mm t ≤ 8mm | Int. (A) | 150-170 | ||||||
Volt. (V) | 21-23 | |||||||
FW t > 8mm | Int. (A) | 180-220 | 170-190 | 200-220 | 200-220 | 140-180 | ||
Volt. (V) | 23-25 | 23-24 | 23-25 | 23-25 | 23-24 | |||
ø 1,6 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||
| FW t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||
M1070
Solid Aluminium-Magnesium welding wire for GMAW (MIG) and GTAW (TIG) welding of aluminium alloys.
Excellent surface finish and very good weldability. Metal fabrication, water piping systems, and electrical components.
EN ISO 18273 | S Al 1070 (Al 99,7) |
|---|---|
AWS/SFA-5.10/5.10M | ER 1070 |
UNS | - |
ISO TR 17671-4 / EN 1011-4 | - |
ASME IX | EN AW-1070A |
CE N. 0035-CPR-C616
Requirements according to EN ISO 18273. The individual values shown in the table are maximum values.
Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti | Be | Al |
|---|---|---|---|---|---|---|---|---|---|
0,20 | 0,25 | 0,04 | 0,03 | 0,03 | - | 0,04 | 0,03 | 0,0003 | 99,70 |
The mechanical properties of the deposited weld metal are influenced by dilution with the base material.
Gas | Temp. | Condition | 0.2% Yield Strength | Tensile Strength | Elongation | |
|---|---|---|---|---|---|---|
Values according to DIN 1732-3 | I1 | 20ºC | As welded | - | ≥ 60 N/mm2 | ≥ 35% |
Suitable for welding 1000 series aluminium alloys. May also be used with 5000 series and other aluminium alloys where leak-tight joints are required and no mechanical property requirements apply.
Product | Diameter (Ø mm) |
|---|---|
Plastic spools, basket spools and packs | GMAW: 1.20 - 1.60 mm GTAW: 2.4 - 3.2 mm |
Store in a clean, dry environment protected from moisture and contamination. After opening the package, if the material is not used completely, keep it in its original closed packaging and preferably in a heated storage cabinet at a temperature of at least 20°C (68°F). The spool label (GMAW) or package label (GTAW) should be retained for product traceability.
Remove the aluminium oxide layer, contaminants (grease, dust, etc.), and moisture from the welding area by mechanical cleaning or brushing with a stainless steel wire brush. Do not machine bevels using oil-based lubricants.
For GMAW (MIG) welding, wire guides (liners, conduits, etc.) and drive rolls must be suitable for aluminium applications and maintained in a clean condition. Avoid striking the gas nozzle.
Thickness | Temperature | |
|---|---|---|
Preheating | ≥ 10 mm | Initial: 90-110ºC |
Interpass Temperature | All thicknesses | Max. 110ºC |
Inert Gas: 100% Ar, Ar-He mixture
EN ISO 14175: I1
Gas Flow Rate: 14-18 L
| | | | | | |
|---|---|---|---|---|---|---|
EN ISO 6947 | PA | PB | PC | PD | PE | PF |
ASME IX | 1G | 2F | 2G | 4F | 4G | 3G ↑ |
GMAW: Direct current, electrode positive (DCEP / DC+). Applicable in both pulsed and non-pulsed transfer modes.
GTAW: Alternating current (AC). Applicable in both pulsed and non-pulsed welding modes.
These parameters may vary depending on the power source and welding procedure used.
ø 1,0 mm
Union | Param.* | Welding positions | |
|---|---|---|---|
All positions | |||
| BW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
| FW t ≤ 3mm | Int. (A) | 110-130 |
Volt. (V) | 20-22 | ||
ø 1,2 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t ≤ 3mm | Int. (A) | 140-150 | - | 140-150 | - | 140-150 | 130-140 |
Volt. (V) | 21-22 | - | 21-22 | - | 21-22 | 21-23 | ||
| BW mb t > 3mm t ≤ 8mm | Int. (A) | 160-180 | - | 150-170 | - | 150-170 | 140-160 |
Volt. (V) | 22-24 | - | 21-23 | - | 21-23 | 23-24 | ||
BW mb t > 8mm | Int. (A) | 180-220 | - | 170-180 | - | 180-220 | 140-200 | |
Volt. (V) | 23-25 | - | 23-24 | - | 23-25 | 23-24 | ||
| FW t ≤ 3mm | Int. (A) | 130-140 | |||||
Volt. (V) | 21-23 | |||||||
FW t > 3mm t ≤ 8mm | Int. (A) | 150-170 | ||||||
Volt. (V) | 21-23 | |||||||
FW t > 8mm | Int. (A) | 180-220 | 170-190 | 200-220 | 200-220 | 140-180 | ||
Volt. (V) | 23-25 | 23-24 | 23-25 | 23-25 | 23-24 | |||
ø 1,6 mm
Union | Param.* | Welding positions | ||||||
|---|---|---|---|---|---|---|---|---|
PA 1G | PB 2F | PC 2G | PD 4F | PE 4G | PF 3G ↑ | |||
| BW mb t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||
| FW t > 5mm | Int. (A) | 280-330 | |||||
Volt. (V) | 26-29 | |||||||